
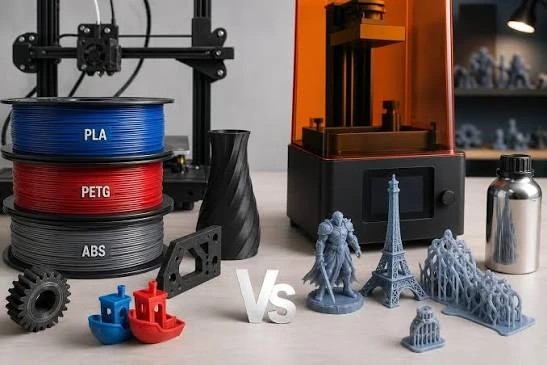
One of the first questions anyone asks before buying a 3D printer is whether to go with FDM (Fused Deposition Modeling) or resin (SLA/MSLA) technology. Both are mature, affordable, and widely used in India today. They solve different problems, though, and choosing the wrong one usually means months of frustration before you switch.
This guide compares the two on the factors that matter in daily use: what you are making, how much detail you need, how much post-processing you can tolerate, and where the machine will sit.
How Each Technology Works
FDM printers melt a thermoplastic strand and deposit it layer by layer through a heated nozzle. Think of it as a very precise, computer-controlled hot glue gun. Typical layer heights range from 0.1 mm to 0.3 mm.
Resin printers use a UV light source, usually 405 nm, to cure liquid photopolymer one layer at a time. Most consumer models are MSLA machines, which use an LCD screen to mask the light and cure a whole layer at once. Layer heights commonly sit between 0.025 mm and 0.05 mm, which is why resin prints look so smooth.
Print Quality and Detail
If surface finish and fine detail are your priority, resin wins clearly. Jewellery masters, dental models, miniatures, and small product prototypes with sharp edges and tiny text are where resin performs best. Layer lines are nearly invisible to the naked eye.
FDM prints show visible layer lines, especially on curved surfaces. For functional parts such as brackets, enclosures, jigs, fixtures, and mechanical prototypes, that rarely matters. You can also reduce layer visibility with a smaller nozzle, lower layer heights, or light sanding.
Rule of thumb: if the part will be looked at closely, consider resin. If it will be used, mounted, or stressed, consider FDM.
Material Options
Material choice often decides the question for you.
FDM offers the widest range of engineering-friendly plastics. A good stock of 3D printer filament can include:
- PLA: easy to print, rigid, low warping. Ideal for beginners, display models, and educational projects.
- PETG: tougher and more heat- and moisture-resistant than PLA. Good for functional and outdoor parts.
- ABS/ASA: strong and heat-resistant, but needs an enclosure to prevent warping and to manage fumes.
- TPU: flexible, rubber-like parts such as gaskets, phone cases, and grips.
- Nylon and carbon-fibre blends: high-strength engineering applications.
Resin also has variety. Standard, ABS-like (tougher), water-washable, flexible, high-temperature, and castable formulations are all available. Choosing the right 3D printer resin matters because standard resins can be brittle. For snap-fits or parts that take impact, a tough or ABS-like resin is usually a better choice.
Build Size and Print Speed
FDM printers generally offer larger build volumes for the money. Printing a 25 cm helmet or a large architectural model in one piece is straightforward on many mid-range FDM machines.
Resin printers cure a full layer at once, so print time depends on part height, not on how many parts are on the plate. Filling the build plate with ten small parts takes about as long as printing one. That makes resin very efficient for batches of small, detailed items.
Post-Processing: The Hidden Time Cost
This is where many new users get surprised.
FDM post-processing is usually simple: remove supports, and optionally sand or paint.
Resin post-processing is a mandatory multi-step workflow:
- Remove the print from the build plate while wearing nitrile gloves.
- Wash it in isopropyl alcohol (90%+) or water, if you use water-washable resin.
- Remove supports carefully.
- Post-cure under UV light to reach full strength.
Uncured resin is a skin and eye irritant, so you need gloves, safety glasses, and good ventilation. Plan for a dedicated workspace, not the dining table.
Running Costs
Entry-level FDM and resin printers now cost roughly the same in India. The running costs differ:
- FDM: filament is the main consumable. Nozzles and build surfaces wear out occasionally.
- Resin: resin costs more per kilogram than PLA. You also need IPA or another cleaning fluid, gloves, paper towels, and periodic replacement of the FEP film and, eventually, the LCD screen.
For large, chunky parts, FDM is usually cheaper per print. For small, detailed parts, the difference narrows because resin uses very little material.
Which One Should You Choose?
| Your priority | Better choice |
| Functional parts, jigs, fixtures | FDM |
| Large prints | FDM |
| Classroom or beginner use | FDM (PLA) |
| Jewellery, dental, miniatures | Resin |
| Batches of small detailed parts | Resin |
| Smooth surfaces with minimal finishing | Resin |
Many workshops and design studios end up running both: FDM for prototyping and functional testing, resin for final presentation models and fine-detail work.
Final Thoughts
There is no universally “better” technology, only a better fit for your work. Start by listing the five parts you expect to print most often. If most of them are functional or large, start with FDM. If most of them are small and detail-critical, start with resin. Choosing based on your real use case, rather than specifications alone, saves both money and frustration.